
Board type
Cement-based, calcium silicate, fibre-cement, MgO-based or another route.
Board Materials & Applications
What manufacturers should confirm before selecting equipment for a fireproof or fire-resistant construction-board project.
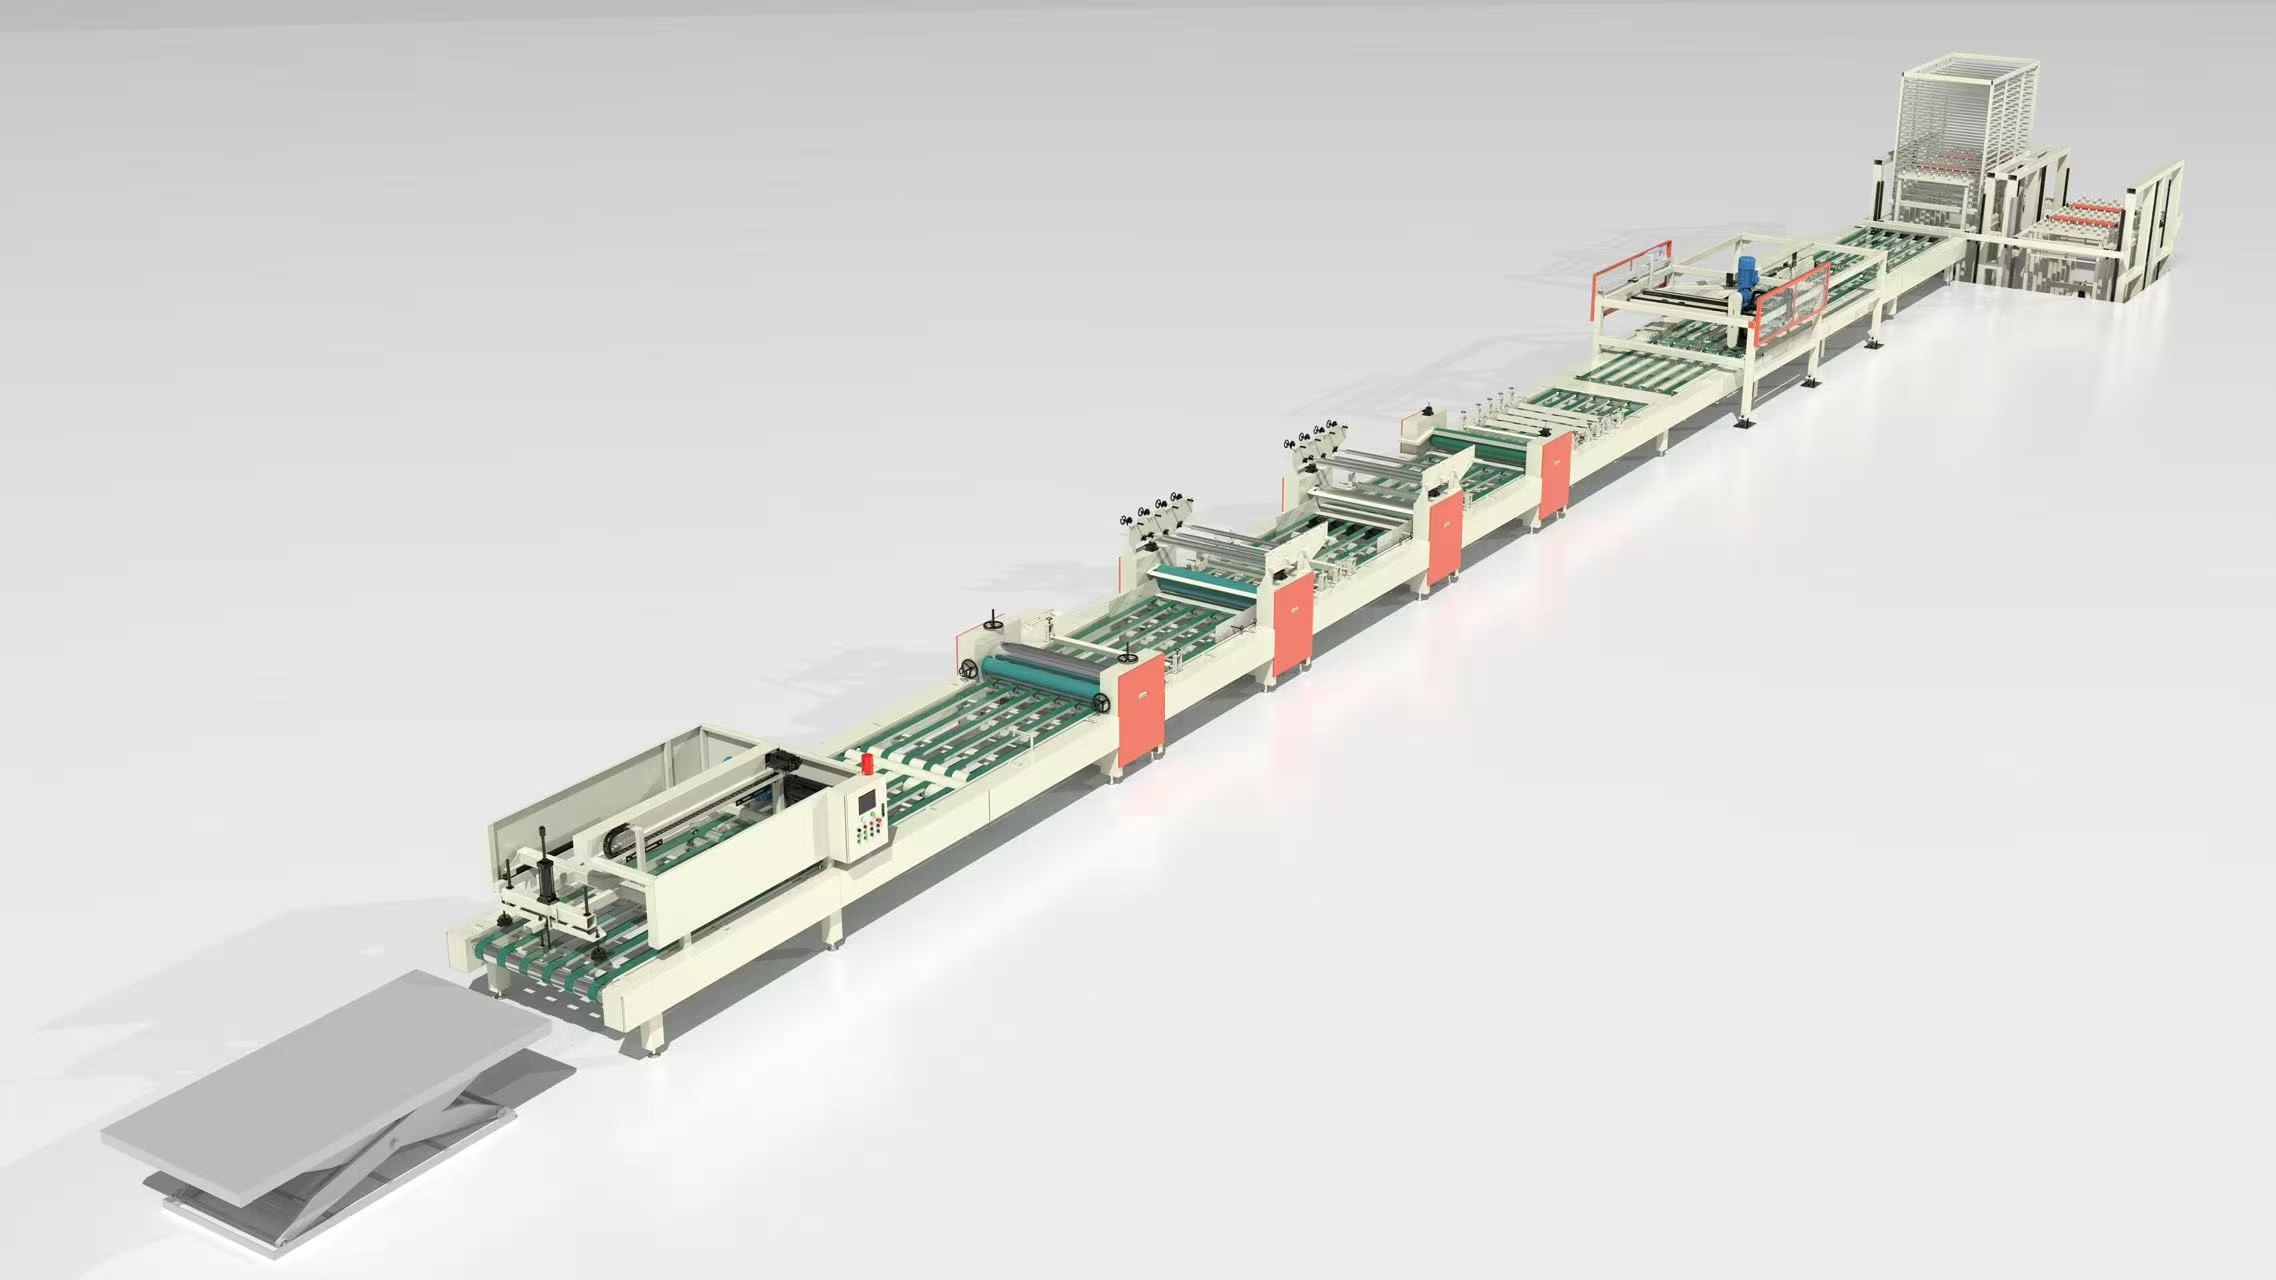
Article summary
Before selecting machinery, define the intended board type, building application, target market, testing route and operating conditions.
Fire performance depends on the complete board or installed assembly, its composition, dimensions, installation method and test conditions. It should not be promised simply because a line includes specific machines.
01 — Performance and end-use application
The first question is not “Which machine makes fireproof board?” It is “What must the finished board or installed system achieve in its target market?” Clarify whether the project involves a board material with a defined reaction-to-fire requirement, a wall, ceiling or partition assembly with a fire-resistance requirement, a fire-rated decorative board or a substrate for later finishing.
ISO 834-1:2025 describes a method for determining the fire resistance of construction elements under standardised fire-exposure conditions. ASTM similarly explains that E119 fire tests assess building elements under specified conditions, and that changes in specimen construction or test conditions can affect the result.
Engineering principleA production-line supplier should configure the process around an agreed product brief. It should not claim that an untested board, or a different installed assembly, will achieve a particular fire rating.
02 — Finished board specification
A production line can only be configured accurately when the product definition is clear. A board designed as an internal partition substrate may require a different process route from one designed for decorative wall panels or other building applications.
Cement-based, calcium silicate, fibre-cement, MgO-based or another route.
Length, width, thickness and allowable dimensional variation.
Density or weight range where applicable.
Raw, sanded, coated, laminated or decorative condition.
Machining, edge condition and final sizing expectations.
Stacking, packaging and finished-product handling.
If the factory will produce several board types, identify which variables can change within one line and which changes require different tooling, process conditions or additional equipment sections. Before discussing machinery, prepare a building board production line planning guide covering the product, capacity, factory conditions and acceptance priorities.
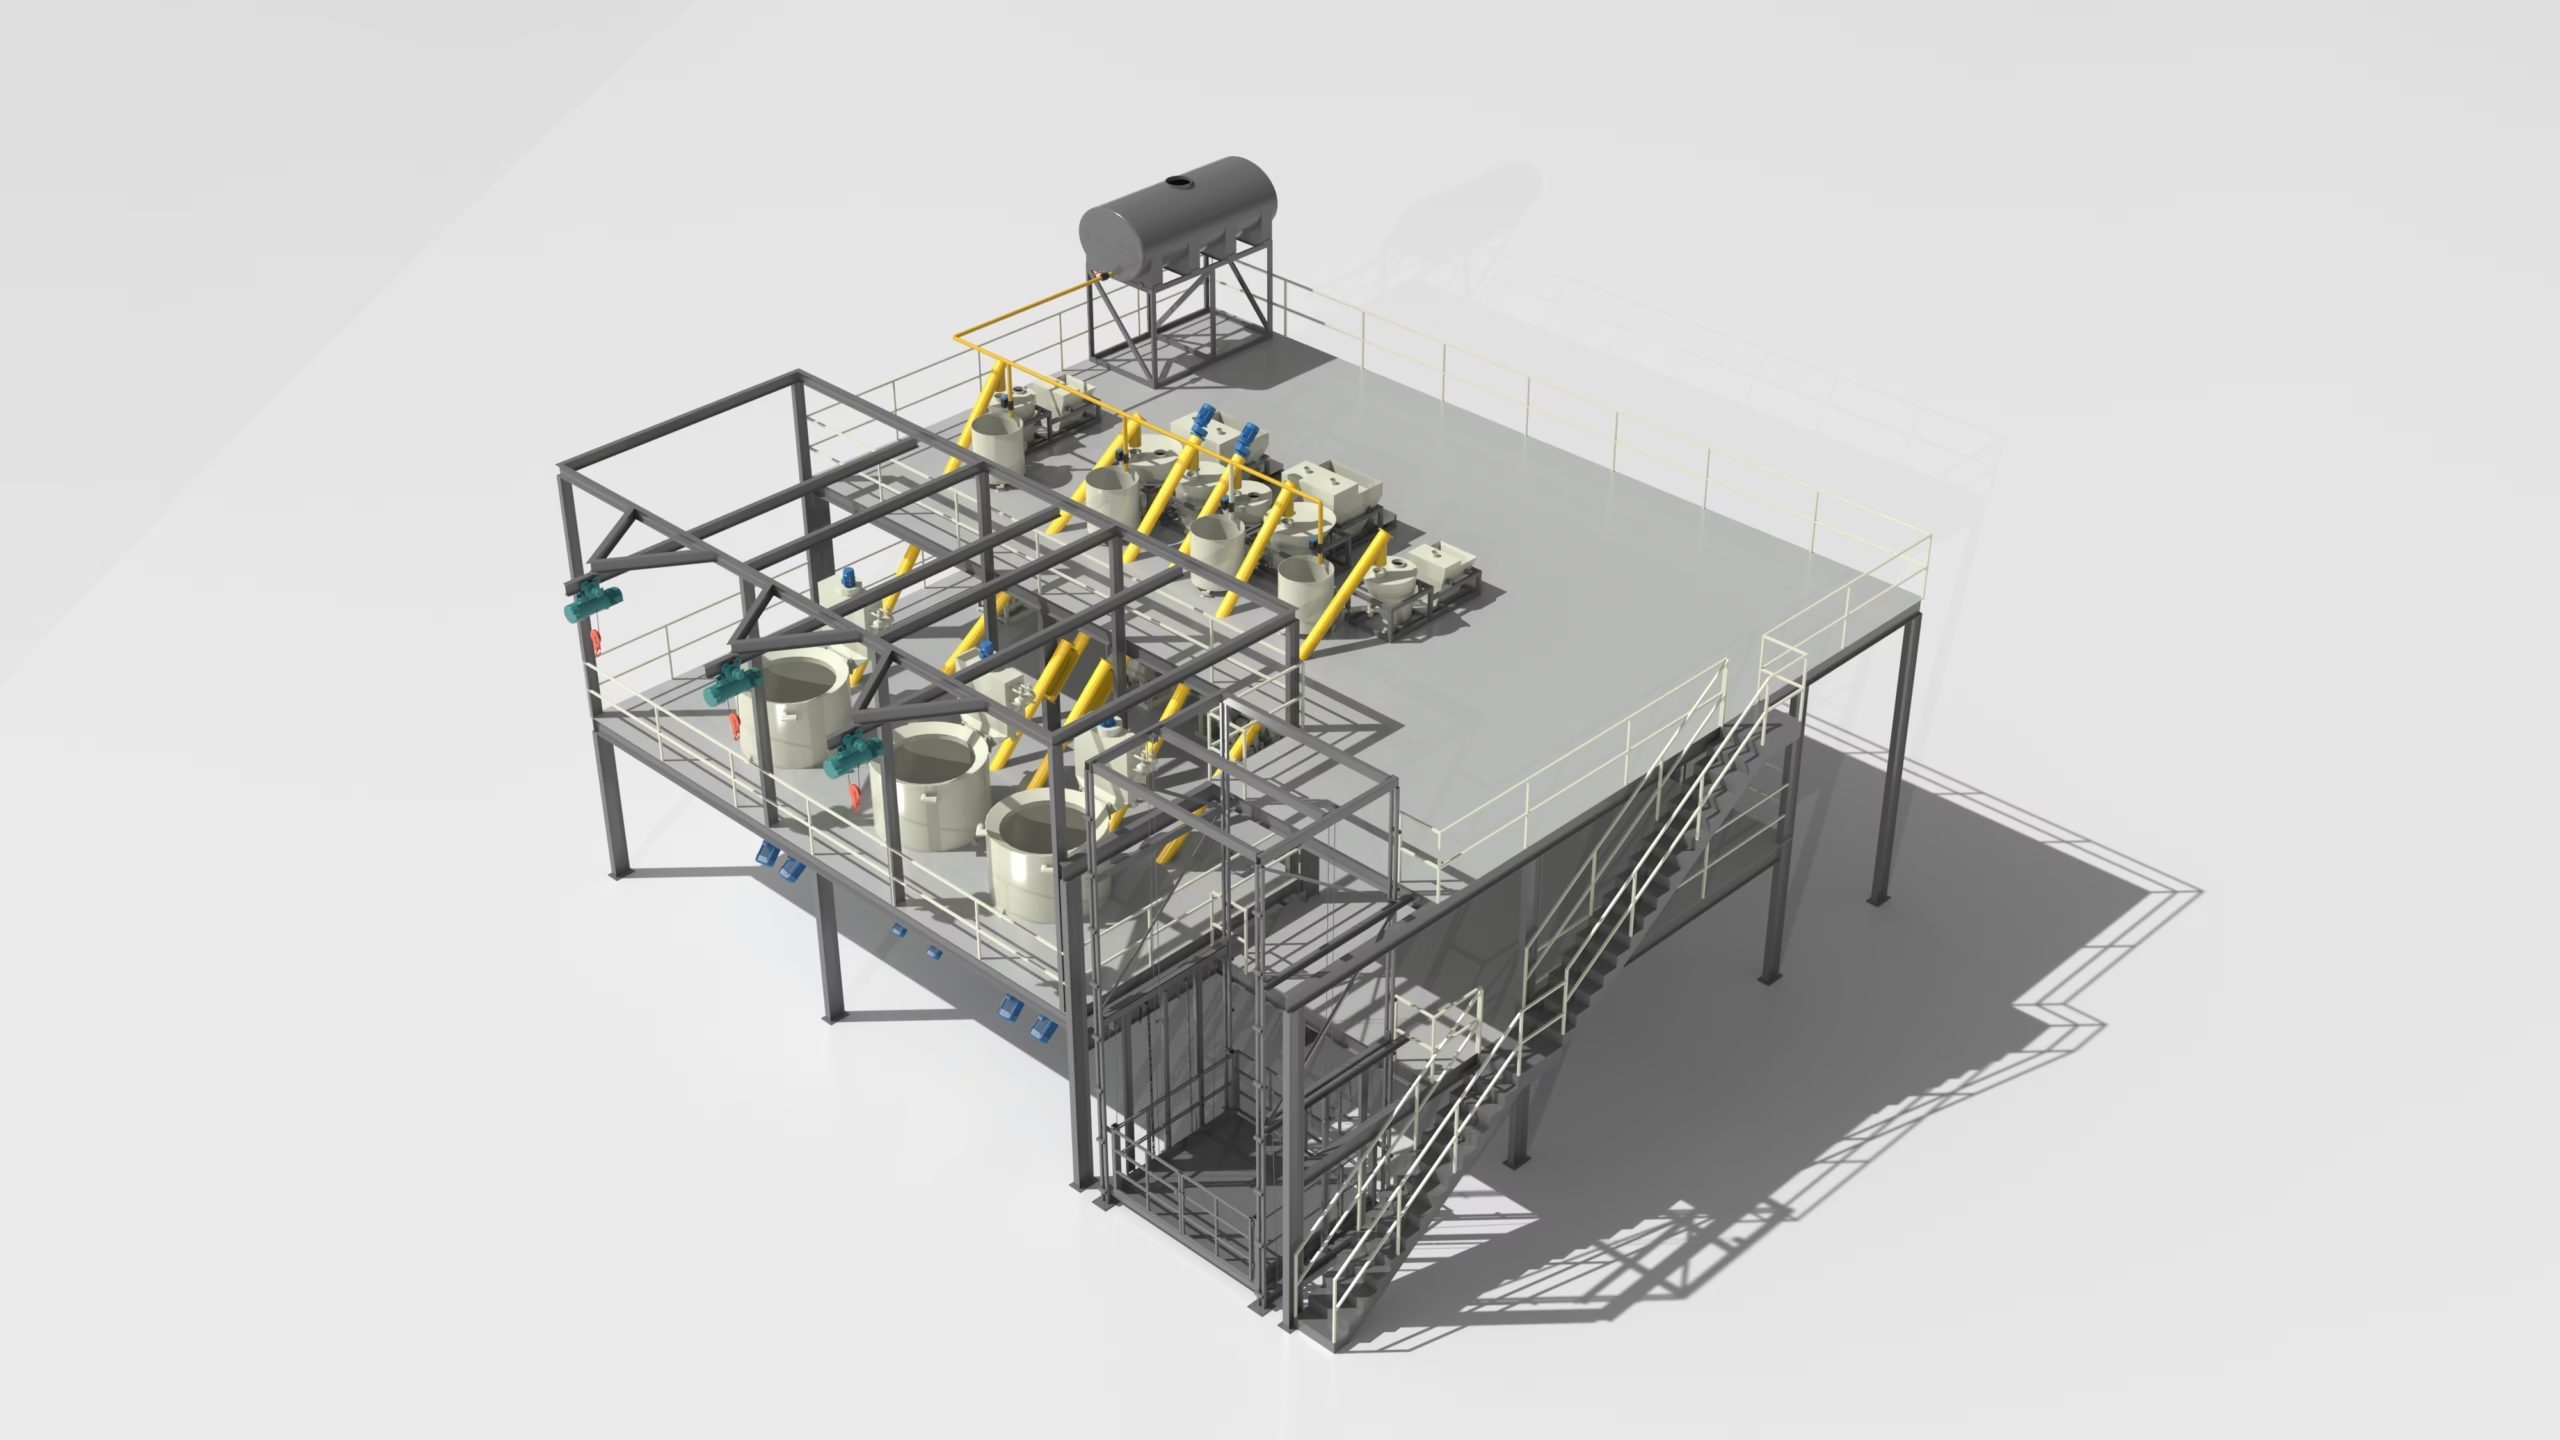
Storage, conveying, weighing, dosing, mixing and dust management must match the actual formulation route.
03 — Raw materials and mixing
Raw-material preparation is the foundation of stable board production. Identify the main binder, fillers, fibres, additives, moisture-sensitive materials and delivery form, including whether materials arrive in bags, bulk containers, silos or another format.
Storage: Delivery form, environmental conditions and usable capacity.
Dosing: Accuracy, batching sequence and traceability.
Mixing: Formula sequence, uniformity and discharge condition.
Dust control: Extraction, containment and operator protection.
Maintenance: Safe access to critical material paths.
Quality control: Checks before material reaches forming.
A feeding and mixing system must match the actual formulation route and the consistency required at forming. Selecting it only by nominal hourly output can lead to uneven preparation, unstable forming conditions or unnecessary manual handling.
04 — Forming and conditioning
Forming is where prepared material becomes a controlled board. The correct board forming system depends on material behaviour, board dimensions, thickness range, production rhythm and the condition required before downstream handling.
Place and shape prepared material consistently across the working width.
Define thickness control, reinforcement and tooling requirements.
Support the board while it remains vulnerable to damage.
Connect material-specific conditioning to the required separation state.
Forming should never be assessed independently from the next production stage. The board must leave forming in a condition downstream equipment can handle consistently. If it is unstable, uneven or difficult to transfer, later sections cannot fully correct the issue.
05 — Downstream processing
After forming and any required material-specific treatment, define the route for board separation, sizing, surface preparation, stacking and optional deep processing.
Separate and support boards without compromising shape or surface.
Match board condition, edge quality and handling direction.
Control thickness and prepare the specified finish.
Check dimensions, surfaces and visible defects.
Protect finished boards through storage and dispatch.
Add finishing after the main production route is stable.
The board cutting equipment should be selected according to board size, target edge quality, material flow and the board’s condition at cutting. Confirm sanding, lamination or grooving before fixing the layout. Deep processing should remain a downstream extension of a stable board-production process.
06 — Factory layout and utilities
A suitable machine configuration still fails if it cannot operate efficiently in the available building. Review the actual dimensions, columns and doors, installation access, storage, utilities, material and personnel flow, maintenance access, inspection space, reject handling and future expansion before freezing the layout.
The objective is a continuous production flow, not simply fitting machinery into empty floor space. A practical layout reduces unnecessary transfers, makes quality checks easier and retains access for maintenance.
07 — Acceptance and project delivery
Before equipment manufacturing begins, agree on the board operating range, trial-production assumptions, scope boundaries, inspection points, factory acceptance requirements, evidence arrangements, site-preparation responsibilities and commissioning scope.
Product basis: Board type, dimensions, surface and range.
Trial basis: Materials and formulation assumptions.
Scope: Equipment, interfaces and process boundaries.
Evidence: Records, videos, samples or inspection.
Site readiness: Foundation, utilities and installation.
Handover: Commissioning, guidance and training.
This turns general expectations into a usable project brief and helps both parties identify missing information before it becomes a delay.
Proposal checklist
With these inputs, an engineering team can assess the complete route instead of recommending isolated machines.
Explore the engineering process →