
Mixing, Forming & Curing
How Feeding and Mixing Affect
Board Quality & Line Stability
Why material identity, dosing, mixing sequence, mixture condition and production rhythm must be controlled before construction-board forming begins.
ARTICLE SUMMARY
Board quality begins when raw materials are received, measured, introduced and mixed.
Variations in material handling and mixing can affect forming behaviour, thickness, surface condition, edge quality and handling stability throughout the line.
The feeding and mixing section must deliver a repeatable material condition to forming—not simply combine ingredients at a nominal hourly output.
01 — DEFINE MIXING CONSISTENCY
Define “consistent mixing”
around the finished board.
A stable mixing process should be defined around the finished-board specification. These inputs allow the engineering team to design a material route that matches the required product instead of selecting a mixer solely by nominal output.
These inputs should already appear in the project’s production line planning guide. For products with a defined fire-performance requirement, the material route should remain consistent with the finished-board specification described in the fireproof board process requirements.
CONTROL PRINCIPLEA change in raw material, formulation, sequence or board structure is a controlled production change—not a minor operator adjustment.
02 — CONTROL MATERIAL IDENTITY
The first quality-control point
is before the mixer.
Materials with similar names or appearance may behave differently in storage, conveying, dosing or mixing. Establish a clear method for receiving, identifying and releasing each material before production.
Approval: Approved material descriptions and supplier records.
Identification: Clear storage locations and batch references.
Handling: Defined instructions for powders, fibres and additives.
Condition: Relevant checks for moisture, contamination or package damage.
Measurement: A documented weighing and dosing method.
Separation: Prevent confusion between similar manually handled materials.
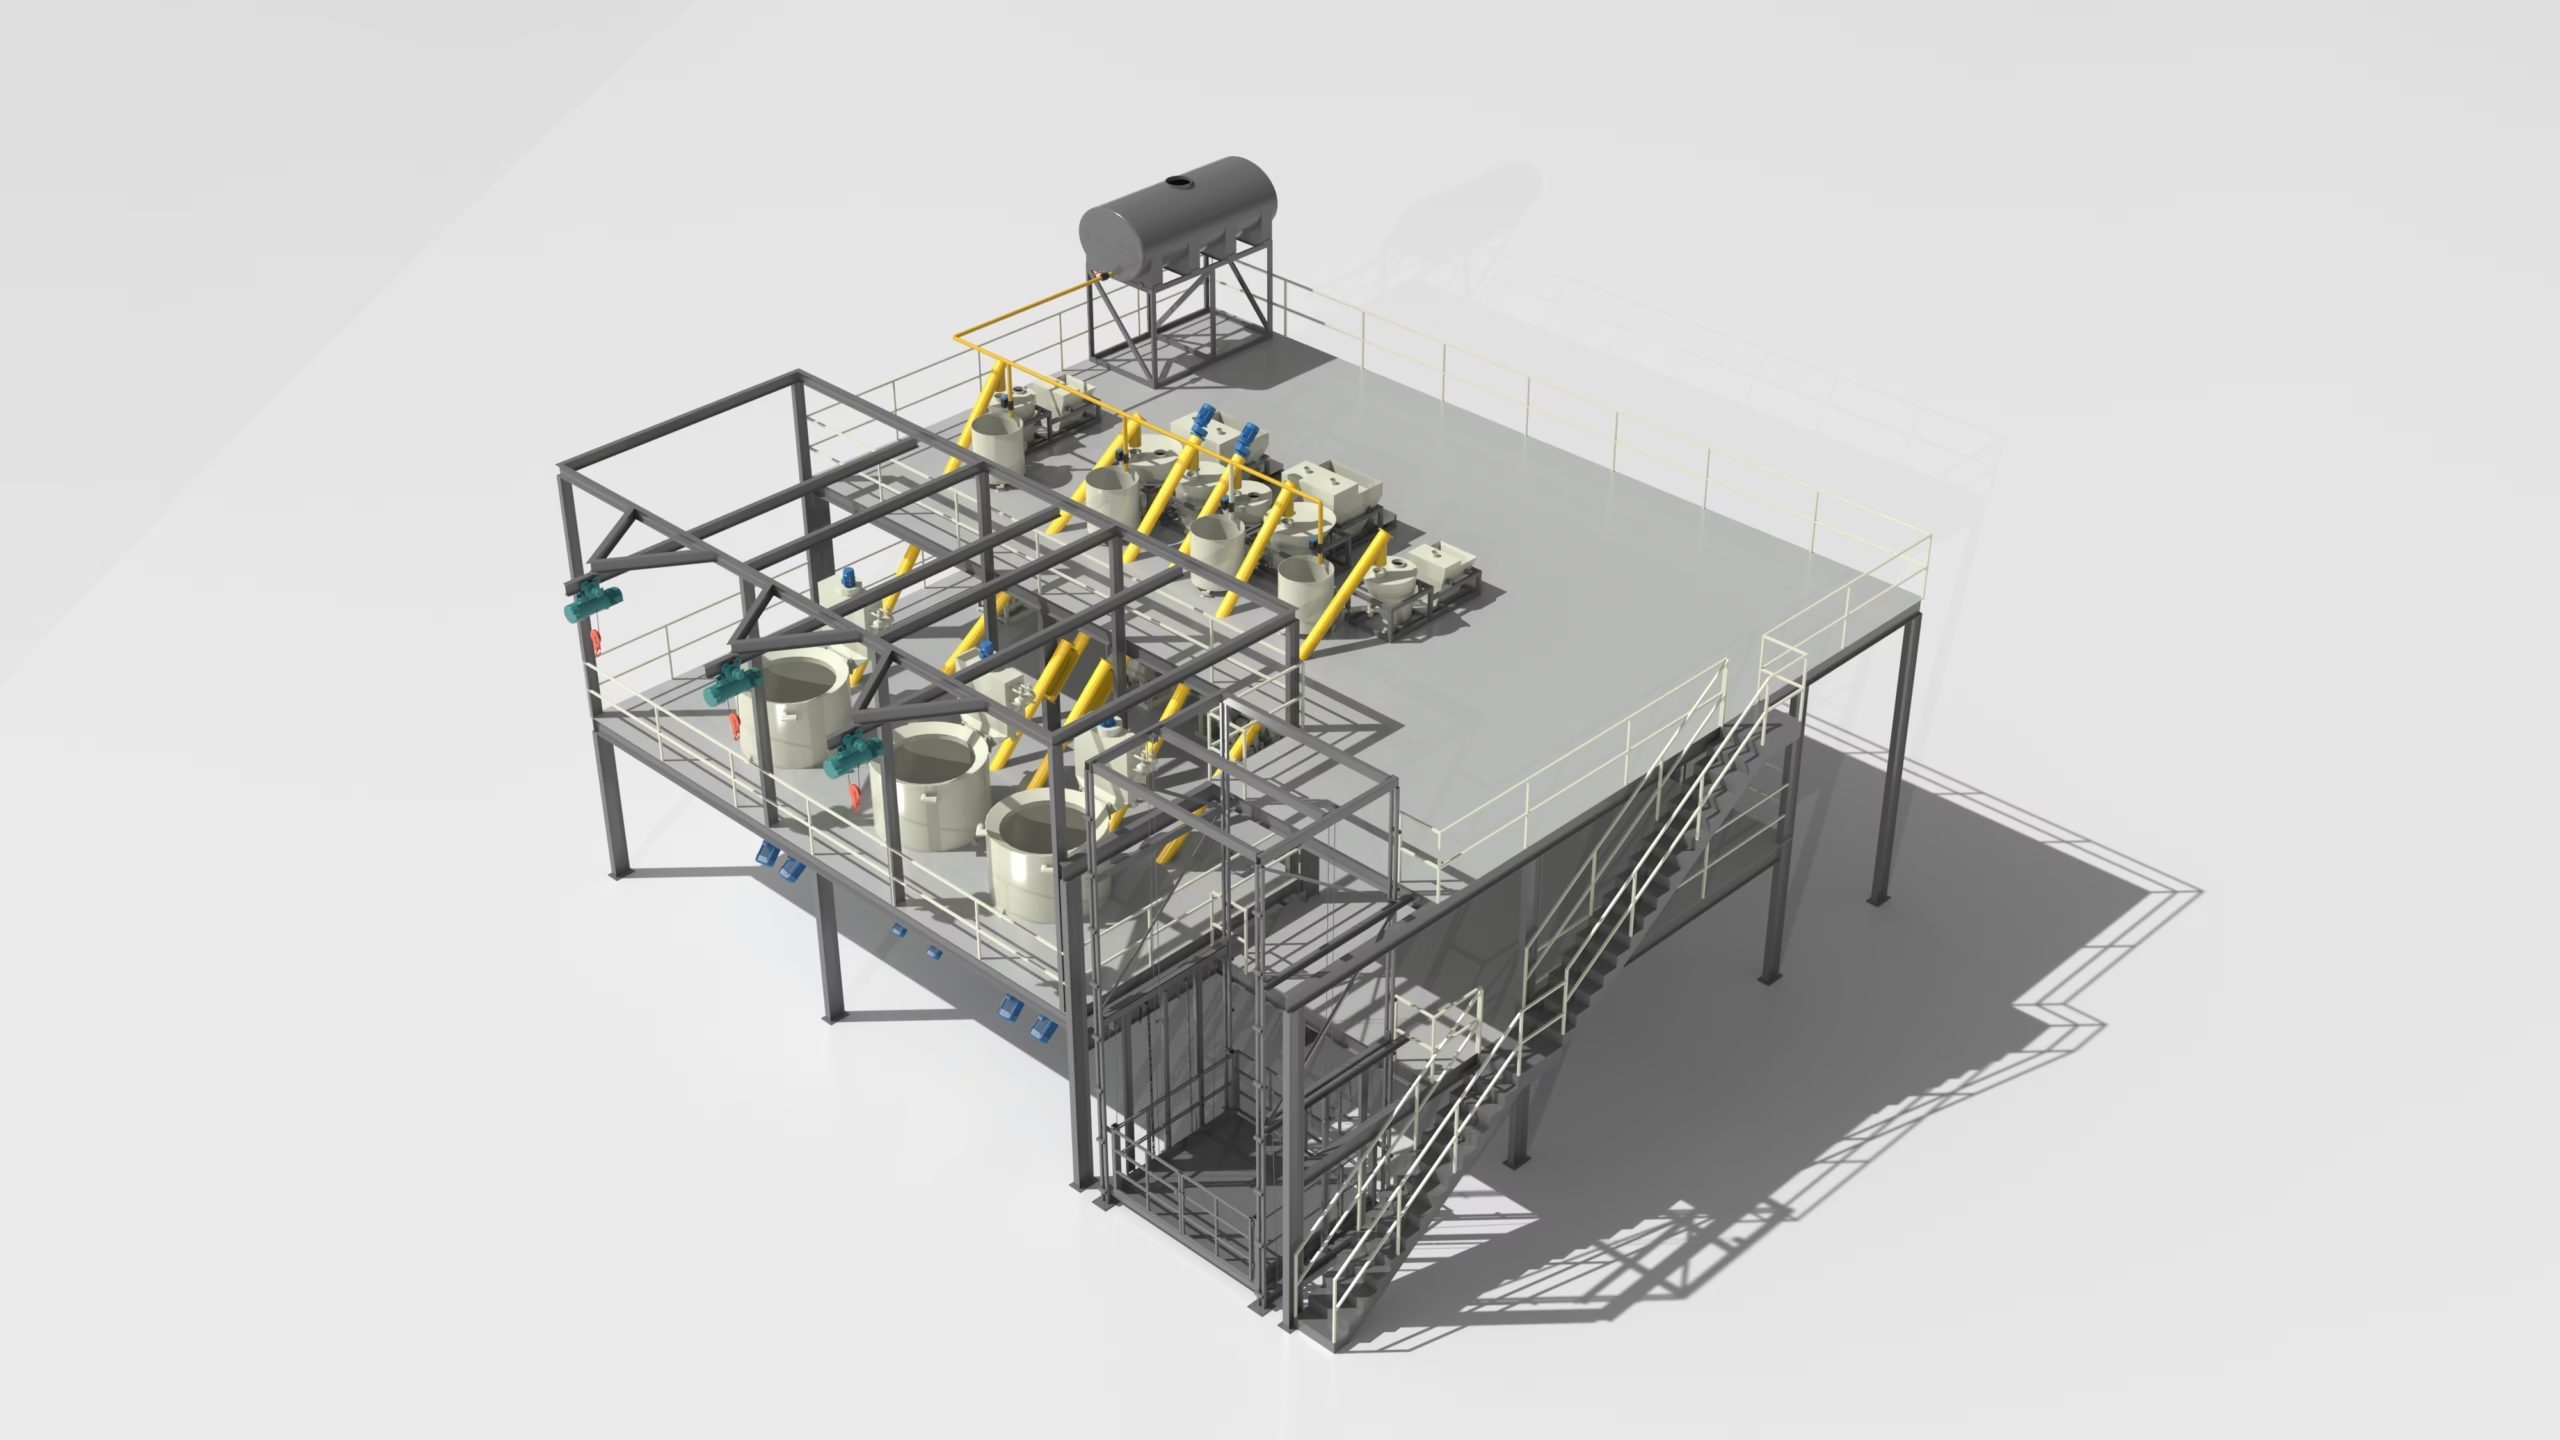
This reduces the risk of using the wrong material, quantity or substitute and makes troubleshooting faster when board conditions change. A feeding and mixing system should follow the actual route: where each ingredient enters, how it is measured, when it is introduced and how it reaches the next stage.
Material identity, dosing accuracy, sequence and transfer condition must remain traceable from storage to forming.
03 — CONTROL MIXING SEQUENCE
Sequence matters as much
as mixing time.
There is no universal sequence for every construction-board formulation. The correct order depends on the material system, fibre type, additives, moisture condition and required process behaviour. Sequence should always be treated as a controlled production parameter.
First ingredients
Define which dry or liquid materials enter first.
Fibre introduction
Define when fibres or reinforcing materials enter the mixture.
One or multiple stages
Document the timing and division of liquid additions.
Stage duration
Set and record how long every mixing stage runs.
Transfer condition
Define the condition checked before material leaves the mixer.
Approval responsibility
Specify who may approve and document a sequence change.
Research on fibre-reinforced cementitious composites has shown that mixing sequence can influence fibre distribution and hardened properties. One study reported improved fibre distribution in its tested system after adjusting liquid-addition and fibre-introduction order. Read the research paper.
04 — MATCH THE FORMING PROCESS
A mixture can look acceptable
and still form poorly.
The material entering forming must match the board geometry, thickness range, handling method and target surface condition. Material that is too dry, too wet, unevenly dispersed or inconsistent between batches may destabilise board formation.
Thickness
Observe whether material variation changes thickness control.
Surface
Check changes in appearance, distribution and uniformity.
Edges
Review whether the mixture supports stable edge formation.
Transfer
Check board stability immediately after forming.
Feeding, mixing and the board forming process should be treated as one connected system. Before repeatedly adjusting forming equipment, first check whether the upstream material condition has changed.
05 — PROTECT PRODUCTION RHYTHM
Line stability depends on timing
as well as material quality.
If material preparation runs faster or slower than forming can accept, the process may create waiting time, inconsistent transfer conditions or manual intervention. The same risk applies when one section stops while another continues producing material.
Normal rhythm: Agreed timing between batching, mixing and forming.
Buffer: Defined capacity where process conditions require it.
Start-up: Coordinated start and stabilisation procedure.
Shut-down: Controlled emptying, stopping and cleaning sequence.
Hold time: Material limits where they are technically relevant.
Interruption: Response and operator communication procedures.
LINE-STABILITY PRINCIPLEA stable line is not one where every machine runs at maximum speed. It is one where each section supports the next at an agreed, repeatable rhythm.
06 — INVESTIGATE VISIBLE SYMPTOMS
Do not assume the final process
is the source of the problem.
Use visible symptoms as prompts to investigate upstream feeding and mixing conditions. These are not automatic diagnoses; production data, material checks and controlled trials must confirm the cause.
| Observed issue | Upstream items to investigate |
|---|---|
| Uneven board surface | Material dispersion, moisture condition, mixing sequence and transfer consistency |
| Thickness variation | Dosing control, mixture condition, forming settings and material flow |
| Inconsistent edge quality | Forming stability, material distribution and board support before cutting |
| Unstable handling after forming | Material condition, curing assumptions and transfer timing |
| Frequent operator adjustment | Batch variation, unclear instructions and missing process records |
07 — BUILD A PROCESS RECORD
A consistent product requires
a consistent record.
For each approved formulation and production route, retain enough operating information for the team to reproduce the process and distinguish material issues from machine, handling or downstream-processing issues.
PRACTICAL STARTING CHECKLIST
Confirm seven inputs before finalising the feeding and mixing configuration.
Finished-board specification and intended application.
Complete material list and storage conditions.
Weighing, dosing and mixing sequence.
Required mixture condition before forming.
Production rhythm between mixing and forming.
Inspection points and process records.
Method for testing and documenting process changes.
With these inputs, the project team can move from a general equipment request to a defined production process. When that agreed process moves to factory testing, use the factory test record checklist to prepare the trial conditions, observations and records needed before shipment.
Review engineering requirements →