
Board Production Planning
Before You Request a
Production Line Quotation
A practical guide to preparing board specifications, materials, output targets, process scope and factory information so your quotation can be reviewed around a clear project basis.
ARTICLE SUMMARY
A useful quotation starts with a useful project brief.
“I need a board production line” is a valid first conversation, but it does not yet define the process route, equipment scope, factory interfaces or acceptance basis.
You do not need every engineering detail before contacting a supplier. Share what is known, identify what remains open and give the team a basis to review assumptions before equipment scope is fixed.
01 — BUILD A QUOTATION-READY INQUIRY
Give engineering a clear
starting point.
A quotation-ready inquiry connects the product you intend to make with the conditions under which the factory must make it. The first review should be able to identify the intended board, material route, target output, included process sections, site constraints and decisions that still need validation.
Product
Board family, application, dimensions, thickness and surface requirements.
Process
Materials, preparation route, forming method and downstream stages.
Factory
Available space, utilities, material flow and existing equipment interfaces.
Project basis
Output target, operating pattern, automation and acceptance assumptions.
The objective is to define a connected production route that can be reviewed, configured and delivered around the actual project. If you are still exploring the concept, begin with a project requirement review before selecting individual machines.
HOW TO HANDLE OPEN ITEMSMark uncertain information as “to be validated.” A visible open question is a better design input than an assumption that changes after the scope is fixed.
02 — DEFINE THE FINISHED BOARD
Start with the board
you plan to make.
Board specifications guide material preparation, forming, handling and finishing. Similar product names can represent different process needs, so describe the finished product in terms the engineering team can review.
Fireproof, fibre-cement, calcium-silicate and MgO-based boards can differ in material route, forming condition and downstream processing. A clear finished-board definition helps distinguish the required first-phase equipment from optional future expansion.
03 — DESCRIBE THE RAW-MATERIAL ROUTE
Connect every ingredient
to its handling method.
The first production sections must match the materials the factory can realistically receive, store, measure and prepare. Share the current formula if available, and explain whether it is established, provisional or still under development.
| Information to share | Why it matters to configuration |
|---|---|
| Binders, fillers, fibres and additives | Defines storage, handling, batching and dosing needs. |
| Delivery form | Bagged, bulk, silo or other supply affects receiving and transfer. |
| Moisture sensitivity or dust generation | May influence containment, extraction, cleaning and operating procedures. |
| Formula status | Shows whether the process is established or needs trial validation. |
| Batch or continuous preparation preference | Helps assess a suitable material-preparation concept. |
| Local material constraints | Identifies substitutions or properties that may need testing. |
Connect material information to the agreed production line requirements. Dosing and mixing equipment should be evaluated against the material route as well as the intended output basis.
04 — STATE CAPACITY IN SALEABLE-BOARD TERMS
Make the output target
measurable and comparable.
“High capacity” can mean different things across projects. State the output unit, operating period and assumptions behind the target. Clarify whether the figure describes theoretical machine throughput or finished boards accepted for dispatch.
Output unit: Specify tonnes, square metres, boards or another agreed measure.
Time basis: Define per hour, shift, day or month and the planned operating hours.
Operating pattern: Share shifts, workdays and planned stoppage assumptions.
Product mix: Note board formats, thickness changes and expected changeover frequency.
Available time: Consider cleaning, maintenance, start-up and other planned downtime.
Expansion: Identify whether the project will be built in phases.
This gives the supplier a basis for reviewing line rhythm, bottlenecks, buffer requirements and downstream handling. A fast individual process section does not by itself establish the output of the complete production line.
05 — DEFINE THE PROCESS SCOPE
Describe the line as a route
from input to dispatch.
State which stages belong in the first project phase, which are already available and which may be added later. The precise route depends on the board type, material system and required product condition.
Receiving & preparation
Material receiving, storage, dosing and mixing.
Distribution & forming
Prepare and form material to the agreed board geometry.
Curing or treatment
Include conditioning, curing or treatment where required by the route.
Release & demoulding
Separate, transfer and support boards in the required condition.
Cutting & edge trimming
Define final dimensions and edge requirements.
Sanding & surface preparation
Include calibration or surface preparation as applicable.
Inspection, stacking & dispatch
Specify inspection, packaging, storage and handling interfaces.
Secondary processing
Consider lamination, grooving, profile wrapping or other future operations.
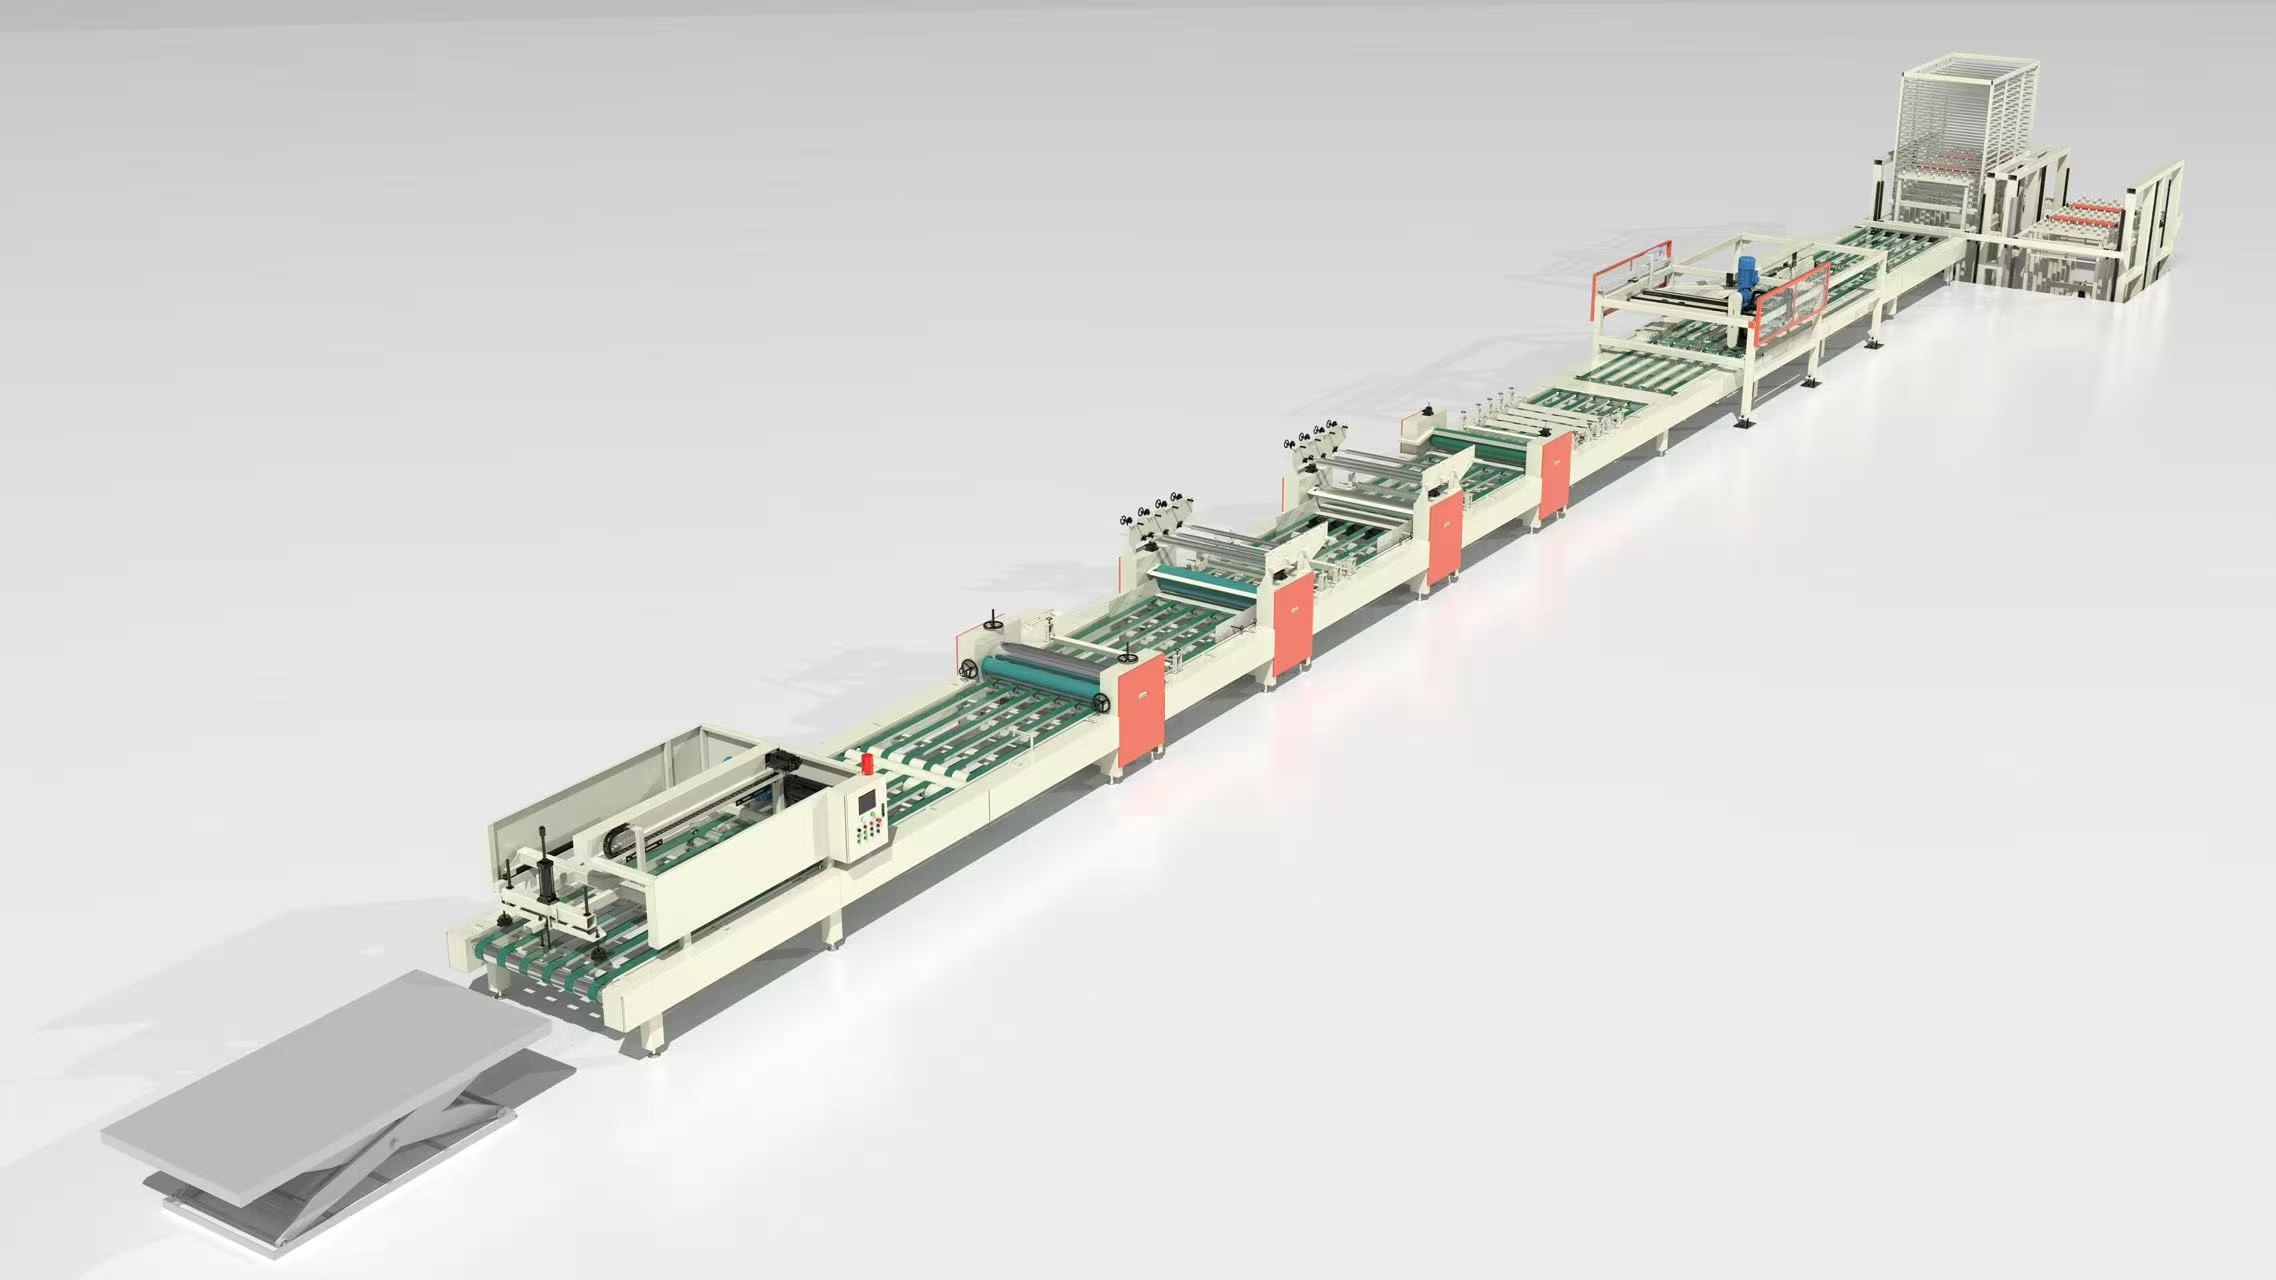
Review the board production machinery portfolio as a process map. Each section must match the board condition it receives and the condition required by the following stage.
06 — SHARE REAL FACTORY CONDITIONS
Check the route against
the building early.
A suitable equipment arrangement still needs to fit the available building, installation access, utilities and material flow. A final construction drawing is not required for an initial conversation; a marked-up plan or clear site photographs can reveal important constraints.
Include utility information only to the level currently known, and mark values that need site verification. Early layout review can help identify access, interface and material-flow questions before the equipment arrangement is finalised.
07 — EXPLAIN THE OPERATING MODEL
Choose automation around
how the factory will run.
Automation should support the actual operating model. Describe the intended balance between manual work, machine assistance and integrated handling so the project team can assess where automation serves a practical purpose.
Staffing
Expected operators by process area and shift.
Handling
Loading, turnover, stacking and transfer requirements.
Controls
Alarms, data, process records and preferred control language.
Changeovers
Product variety, change frequency and cleaning expectations.
Also identify existing equipment interfaces and local operating requirements. This helps establish where integrated handling may be useful and where a simpler arrangement may be easier to maintain.
08 — SET THE ACCEPTANCE BASIS
Agree what will be reviewed
before manufacturing begins.
Discuss the project review basis while configuration decisions are still being made. These points support clear coordination; final responsibilities, criteria and commercial terms should be documented in the project agreement.
Product basis: Board type, dimensions, thickness range and intended operating range.
Material basis: Trial materials, formula status and assumptions requiring validation.
Scope boundary: Included equipment, utilities and interfaces between sections.
Verification: Inspection points, trial conditions and records to be reviewed using the factory acceptance testing checklist.
Site readiness: Civil preparation, utilities and customer-side responsibilities.
Handover: Installation, commissioning, training and documentation scope.
When an item depends on customer materials, site conditions or a later trial, state that dependency explicitly so both teams understand what remains to be confirmed.
09 — AVOID COMMON INQUIRY GAPS
Four missing details can
make early estimates unreliable.
| Inquiry gap | What it leaves unclear | Useful next input |
|---|---|---|
| “We need a complete line” without a board definition | Process route, geometry, surface requirements and downstream condition. | Board family, application, dimensions, thickness and finish. |
| Capacity without shifts or product mix | Operating basis, changeovers, cleaning and expected saleable output. | Time period, shifts, product formats and availability assumptions. |
| Factory layout considered after equipment selection | Access, utilities, material flow and installation constraints. | Basic plan, dimensions, photos and known utility information. |
| Acceptance first discussed near delivery | Trial assumptions, inspection records and project responsibilities. | Early agreement on product basis, verification and handover scope. |
These gaps are normal in an early project. The useful step is to identify them, assign an owner and decide whether they need a site check, material trial or engineering review.
10 — COPY THE FIRST INQUIRY TEMPLATE
Send what you know.
Flag what remains open.
Use this checklist as a starting point for your first engineering discussion. If an answer is not confirmed, write “to be validated” and add any current assumption.
Finished dimensions and thickness range:
Target output and operating shifts:
Main raw materials and formula status:
Required process stages:
Surface, edge and downstream finishing requirements:
Factory location and available layout information:
Available utilities:
Automation and handling preference:
Target project timing:
Open questions for engineering review:
A clear first brief helps the team determine the next engineering questions without asking you to finalise every technical point at the start.
FROM INQUIRY TO PROJECT BRIEF
A useful quotation process clarifies the board, process route, factory conditions and next decisions.
Define the intended finished board.
Describe available materials and formula status.
State saleable output and operating pattern.
Map the first-phase process sections.
Share the available factory plan and constraints.
Discuss verification and handover assumptions early.
For support from requirement definition through configuration, manufacturing, verification and handover, explore building board production engineering.
Start an MGO Equipment project inquiry →