
Board Production Planning
Building Board Production Line
Factory Acceptance Test Checklist
A practical FAT guide for confirming equipment scope, trial conditions, operating functions, records and open items before shipment—while keeping factory testing distinct from site commissioning.
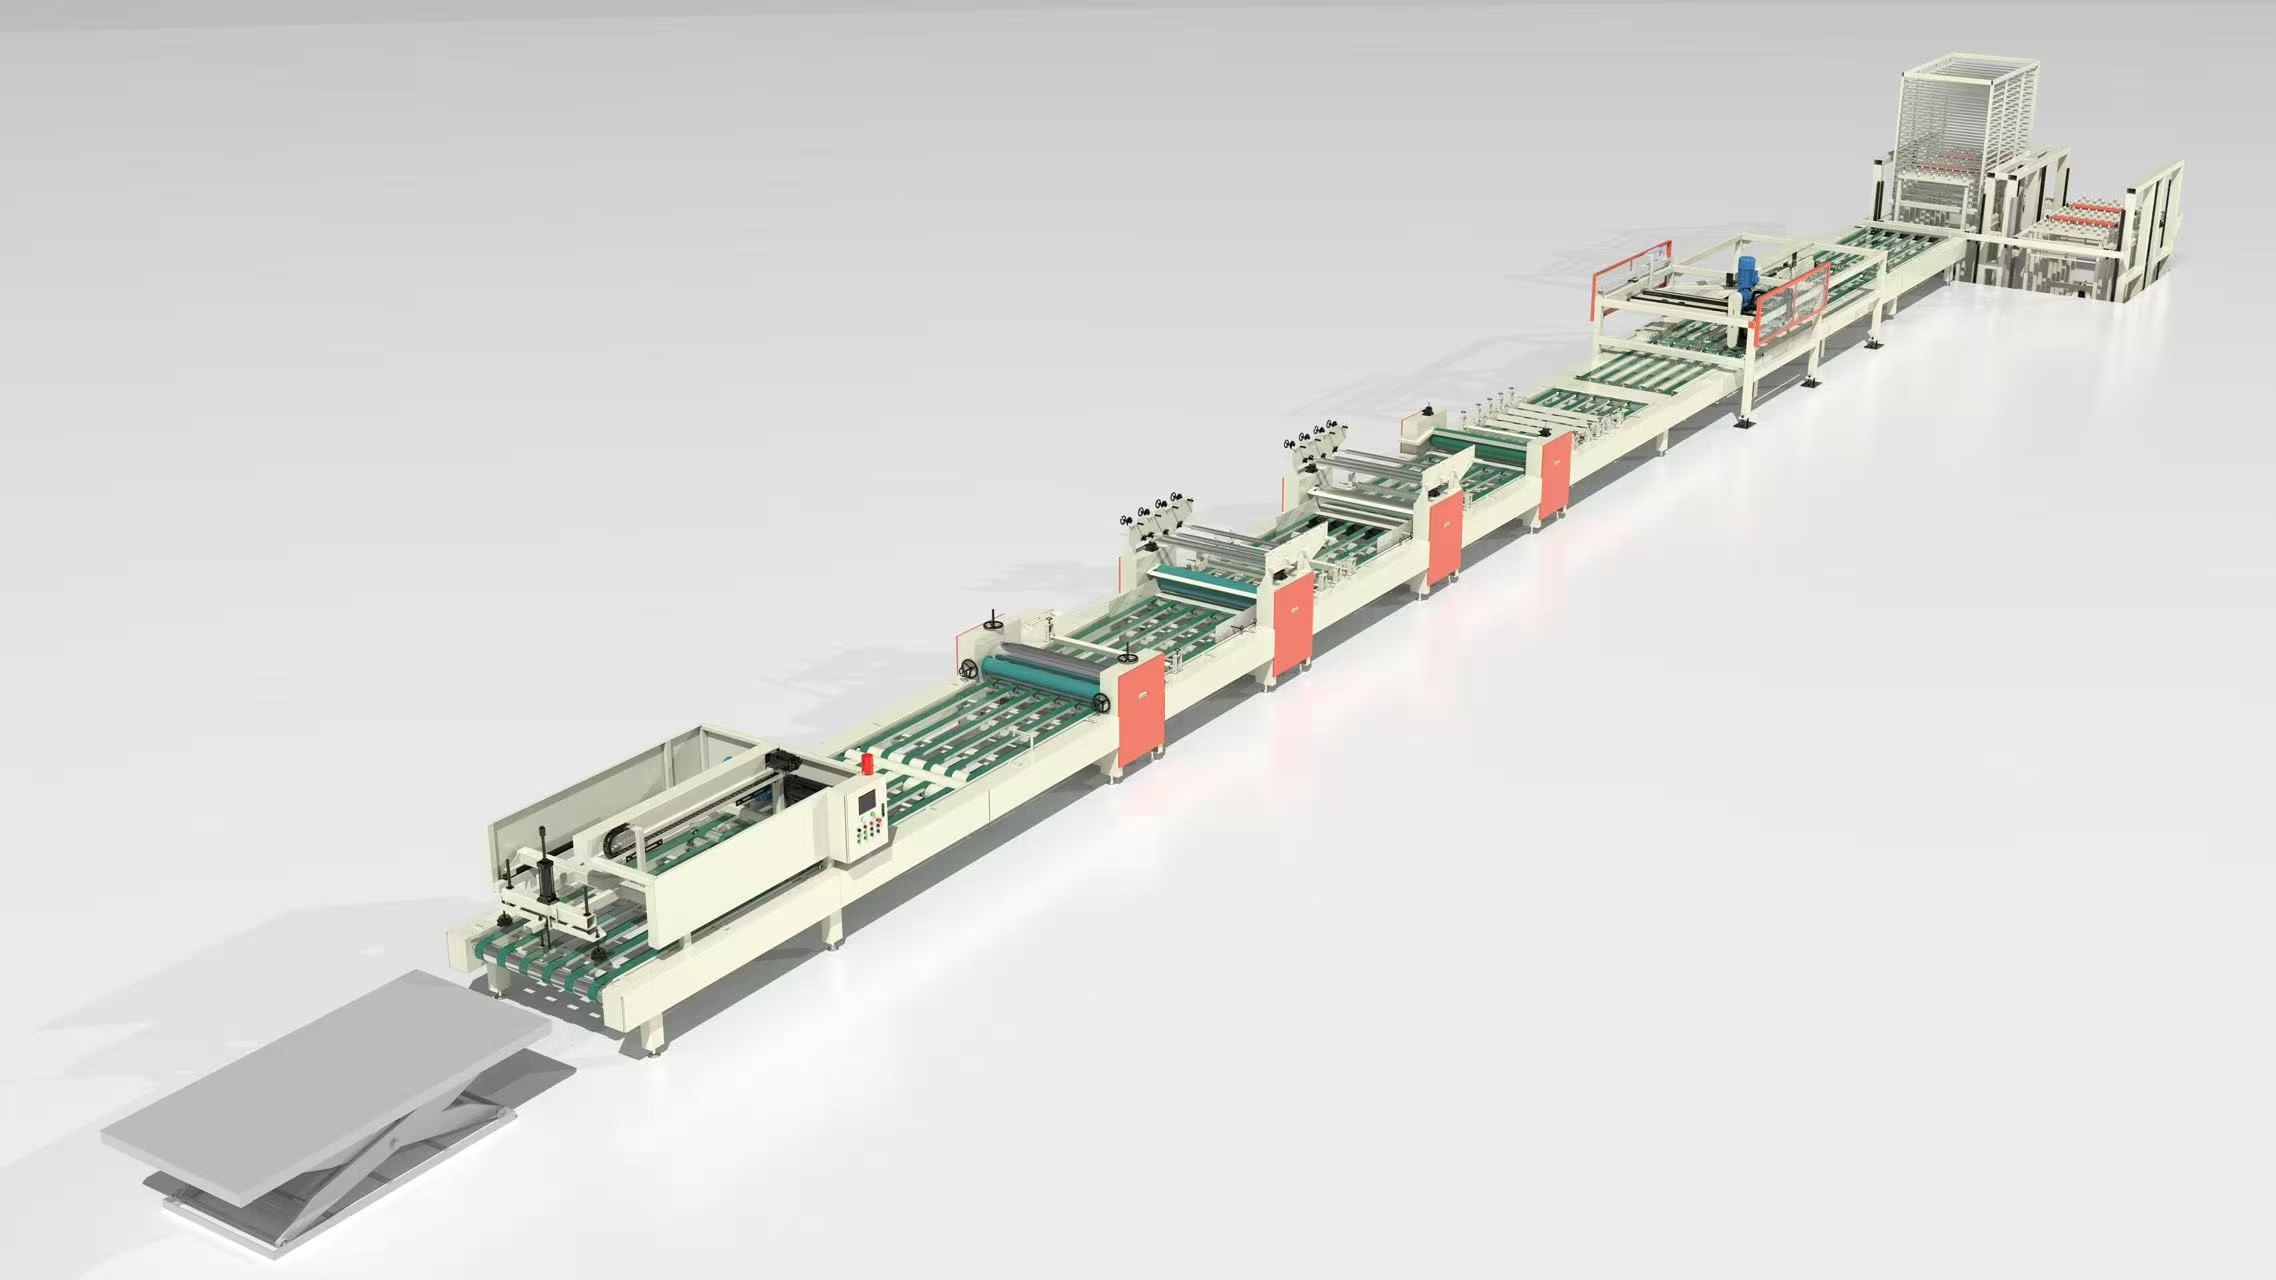
ARTICLE SUMMARY
A factory acceptance test is a structured project review—not just a machine demonstration.
For a building board production line, FAT can verify agreed equipment scope, operating functions, controls and defined trial conditions before shipment.
It cannot replace installation or commissioning at the customer’s site. Agree the evidence, responsibilities and remaining site-dependent actions in advance, then record the results and open items clearly.
01 — DEFINE WHAT FAT MUST CONFIRM
Put the test scope
in writing first.
A project should not rely on an informal assumption that “the line will be tested.” Before scheduling attendees or trial production, document what the factory review is intended to confirm, which equipment is included, what conditions will be available and how findings will be recorded.
The scope should follow the actual supply contract and configuration. A complete production line, one board-forming section and a downstream cutting module have different interfaces and therefore need different acceptance checks.
Review the original requirement before locking the test plan. If board type, dimensions, thickness range, capacity assumptions or optional processing have changed, record the variation and assess whether the agreed test basis must change too. The line quotation checklist can help revisit the original project inputs.
ACCEPTANCE PRINCIPLEEvery test item needs a defined basis: what is checked, under which conditions, what evidence is retained and who confirms the result.
02 — SEPARATE FACTORY VERIFICATION FROM SITE COMMISSIONING
Test what can be proven
at the factory.
FAT and commissioning are connected project stages, but they are not interchangeable. A supplier’s factory can verify agreed equipment and functions under available conditions. It cannot reproduce every customer building, utility connection, material supply or operating routine.
| Factory review may cover | Often requires the customer site |
|---|---|
| Equipment identity and major module configuration | Final building access, layout and installation conditions |
| Mechanical assembly, movement and basic operation | Foundations, installation alignment and final interfaces |
| Agreed control logic and operating sequences | Site electrical, water, air, drainage and extraction connections |
| Conveyor direction and supplied transfer interfaces | Integration with customer-owned upstream/downstream equipment |
| Guarding, emergency stops and accessible controls in supplied scope | Local safety arrangements and site-specific compliance checks |
| Empty-run or defined material trial, if available | Performance with the customer’s actual raw materials and routine |
| Shipment preparation and documentation review | Operator readiness, training and stable production at the site |
List each deferred item with its next verification stage. This prevents a factory observation from being interpreted as proof of final installed performance, and helps the customer prepare the building, utilities and project team for arrival.
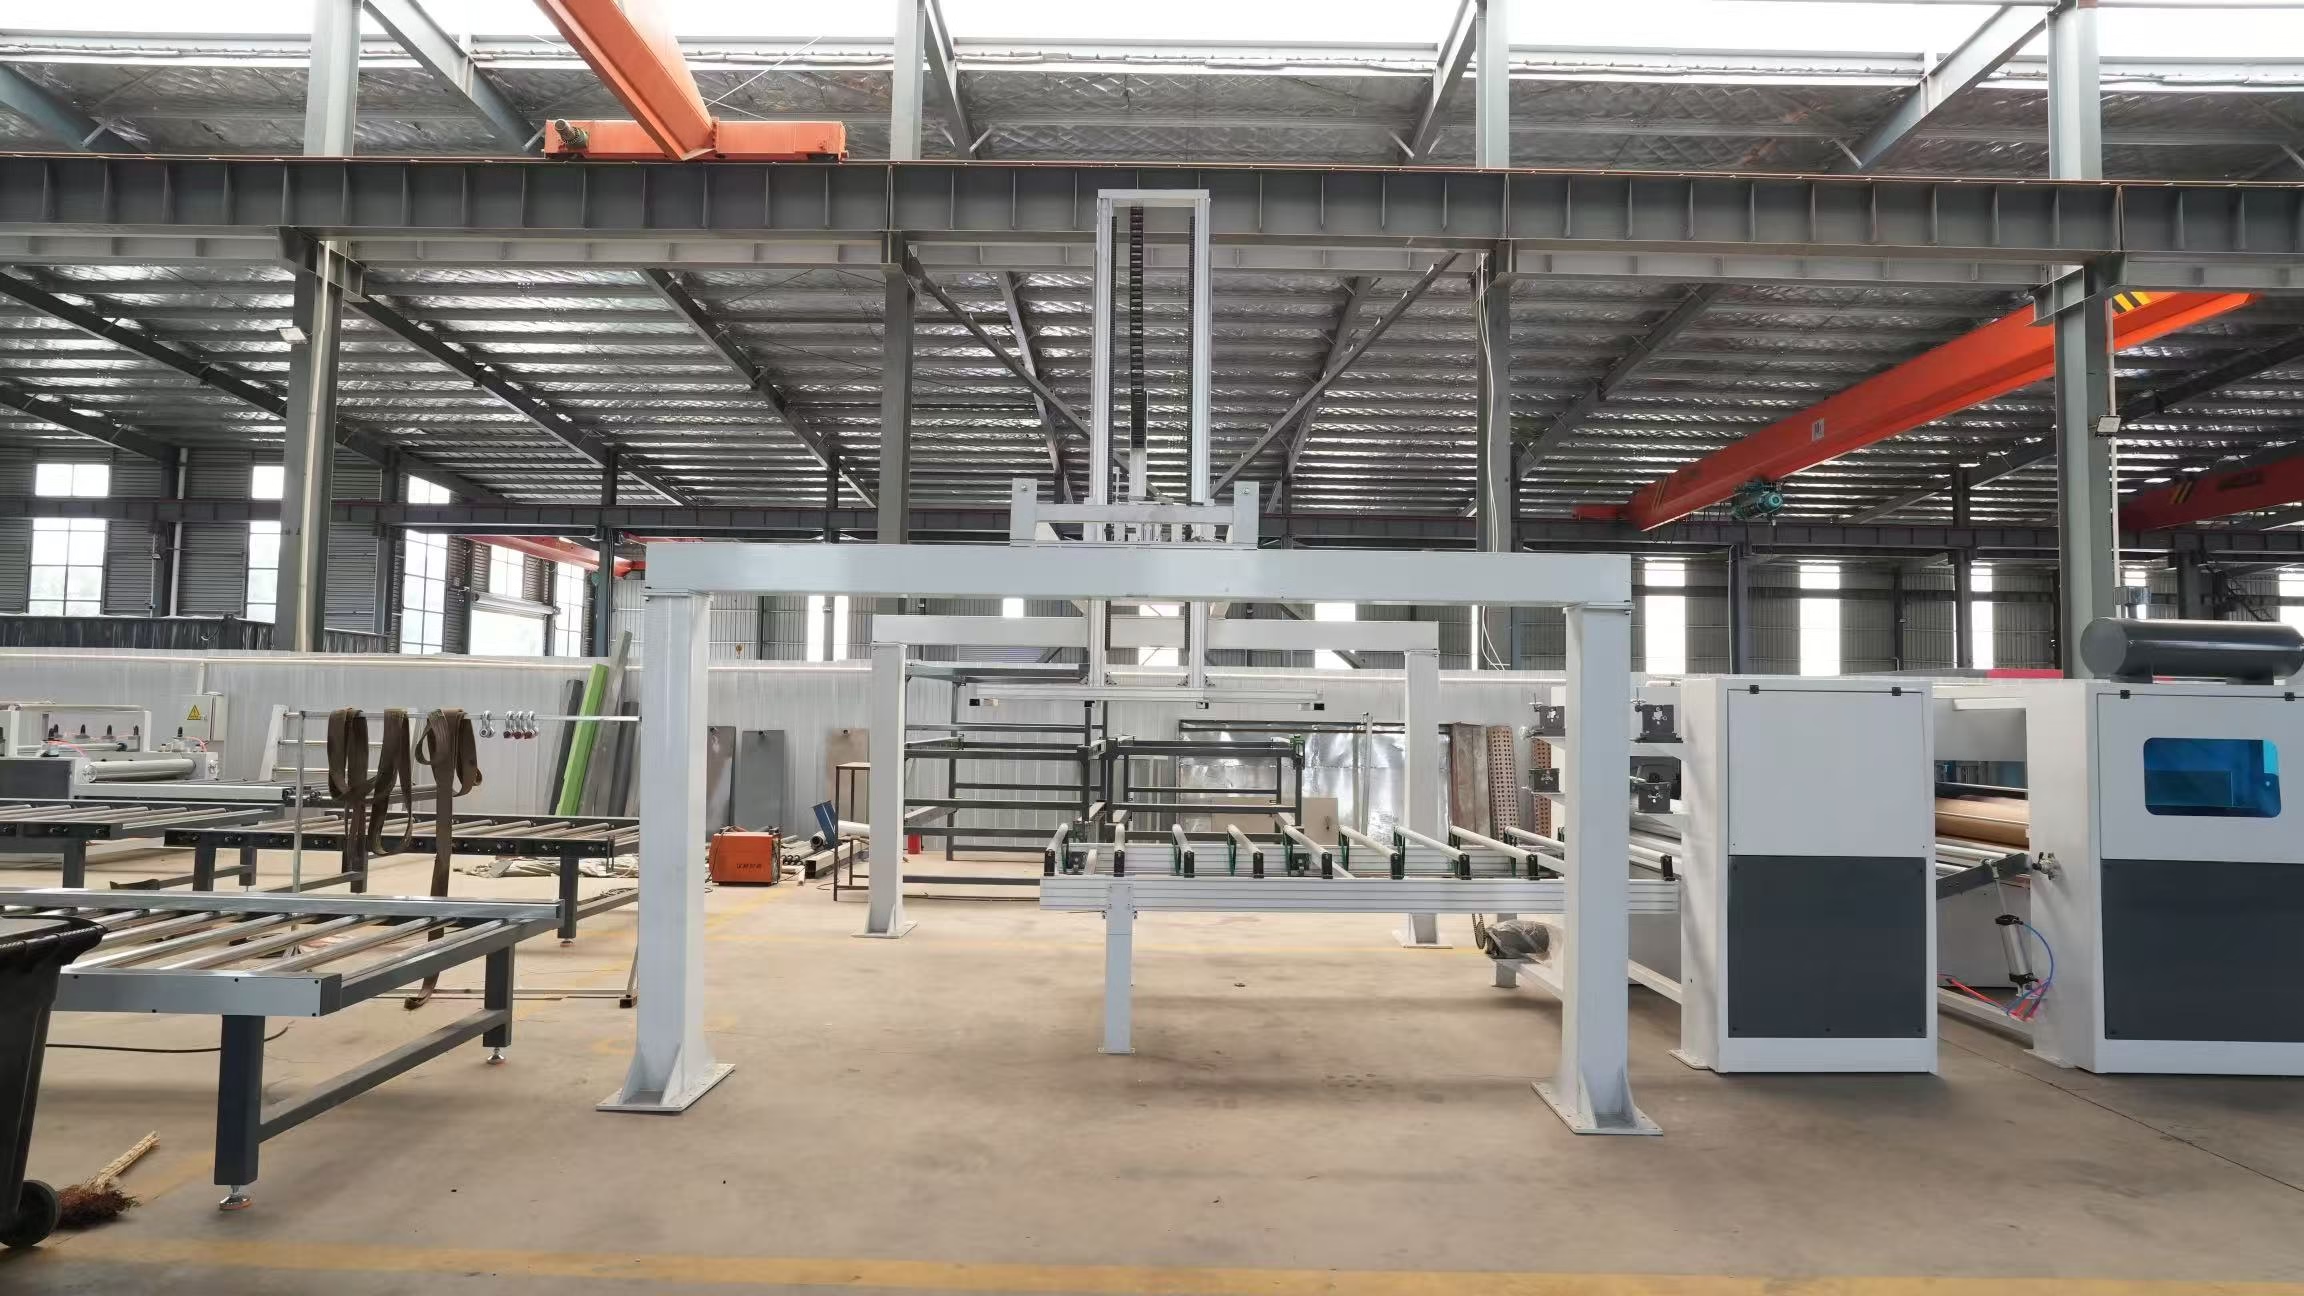
Record the available materials, equipment scope and operating conditions behind every trial result.
03 — CONFIRM THE PROJECT BASIS BEFORE A TRIAL
Give every observation
a clear reference.
A trial without an agreed reference point can produce disagreement rather than useful evidence. Before testing, customer and supplier should confirm which product and process the review relates to, what inputs are available, who is attending and what counts as an open item.
| Project basis | What to confirm | Why it matters |
|---|---|---|
| Equipment scope | Included modules, options, interfaces and exclusions | Sets the boundary of what can be inspected |
| Product basis | Board type, dimensions, thickness range and surface condition | Connects the test to the intended output |
| Trial material | Material availability, agreed substitutes and known limitations | Prevents overstating what a trial represents |
| Process route | Feeding, mixing, forming, conditioning, release, cutting and finishing as applicable | Checks interfaces in the intended sequence |
| Test criteria | Functions, observations, documents and open-item process | Clarifies how findings will be evaluated and recorded |
| Roles | Attendees, record owner and approval/change authority | Gives questions and actions a clear owner |
| Site-dependent items | Checks deferred to installation or commissioning | Creates a practical post-delivery action list |
The acceptance route should remain consistent with the complete board production plan. Test a connected production concept, not an isolated machine result detached from the board, material route and downstream handling requirements.
04 — PREPARE MATERIALS, TOOLING AND CONDITIONS
Make the trial realistic
and repeatable.
A useful factory test depends on preparation. If a material run is planned, agree what material will be used, who supplies it, how much is available, how it will be handled and whether it represents the intended production route. If substitute material is necessary, state the limitation in the record.
Material: list the available raw materials, quantities, condition and any agreed substitutes.
Product target: confirm trial board dimensions, thickness range and relevant surface expectations.
Tooling and handling: identify moulds, belts, pallets, supports or transfer equipment needed for the run.
Operating basis: document agreed settings, recipes or operating sequence where these are within scope.
Inspection: prepare the tools and method used to capture observations and measurements.
Housekeeping: agree cleaning before and after testing and identify any safety restrictions for visitors.
After-test condition: confirm preservation, packing and equipment preparation for shipment.
Do not describe a trial as proof of commercial production performance unless the actual material, product specification and relevant site conditions were represented and the agreed criteria support that conclusion. Record exactly what was tested and identify the next validation step. Confirm options and interfaces against the written equipment scope.
05 — USE A PRACTICAL FAT CHECKLIST
Organise the review
before, during and after.
This checklist is a planning aid, not a universal pass-or-fail standard. Adapt it to the supplied equipment, project contract and agreed trial basis.
Prepare the review
Confirm attendees and responsibilities, equipment scope, relevant drawings, test sequence, materials, tooling, safety arrangements and the record format. Identify which checks must wait for site installation.
Observe and document
Verify major modules; observe start, stop, emergency-stop and normal sequences; review transfers, operator access and supplied interfaces. Record abnormalities, adjustments, limitations and unclosed questions as they occur.
Close the record
Review findings together, assign open items, identify any retest, confirm documents to be issued and agree packing, shipment preparation and installation information.
06 — RECORD OPEN ITEMS CLEARLY
Turn unresolved questions
into owned actions.
An open item is not automatically a failed test. It is a point that has not been fully closed and needs a defined next action. Vague notes such as “to be discussed later” leave the project exposed to different interpretations during packing, delivery or installation.
Keep the record factual and version-controlled. If an adjustment is made during the test, note the original observation, the change and its reason. If a retest is needed, state which condition or function is to be reviewed again and how completion will be evidenced.
07 — BRING THE RIGHT PEOPLE INTO THE REVIEW
Review the line through
more than one lens.
A production line is not meaningfully reviewed by a signature alone. Different participants can identify different risks—product assumptions, process behavior, site readiness, maintenance access and commercial scope. Invite people who can evaluate the project basis and make or route decisions.
Product and process
Confirm intended board, production objective, material assumptions and process route.
Layout and utilities
Review site preparation, access, service interfaces and customer-owned equipment connections.
Quality and maintenance
Consider process checks, operator workflow, routine service and spare-parts planning.
Scope and documentation
Track agreed scope, records, changes, open actions and the handover to installation.
For complex projects, connect FAT preparation to the wider testing and FAT stage so manufacturing verification, project records and site handover remain aligned.
08 — KNOW WHEN FAT IS NOT ENOUGH
Plan separate site validation
where conditions differ.
The factory test should be broad enough to close what can be proven before shipment, but not stretched into claims it cannot support. Final outcomes may still depend on installation quality, utilities, civil works, local raw materials, customer routines and interfaces with other plant equipment.
FACTORY TEST ≠ SITE COMMISSIONINGUse FAT to verify the agreed factory scope and make remaining site work visible, assigned and manageable. Confirm local requirements with appropriately qualified parties.
09 — TURN FAT PREPARATION INTO A CLEAR HANDOVER
Close the factory review
with a usable next-step plan.
A good FAT starts well before the test date. It depends on a defined equipment scope, a representative and honestly described test basis, prepared people and materials, clear records and agreement about what must wait for commissioning.
Agree the basis
Confirm scope, criteria, materials, participants and factory/site boundaries.
Verify what is available
Observe the agreed functions and capture facts, limits and adjustments.
Assign every open item
Set an owner, closure evidence and the next review stage.
Prepare for site work
Transfer documentation and site-dependent actions into installation planning.
If you are preparing a new board-production project, share the intended product, process route, target capacity, factory layout and any required test expectations. These inputs help align testing with equipment configuration and delivery planning.
A BETTER BASIS FOR FACTORY ACCEPTANCE
Verify the agreed scope. Record the evidence. Carry site-dependent work forward.
Define what the factory test is intended to confirm.
Agree the product, material and operating basis for each trial.
Separate factory verification from installation and commissioning.
Assign owners and closure evidence to open items.
Transfer remaining actions into the site handover plan.
Start the discussion with your equipment scope, board requirements and target process route.
Discuss a board production project with MGO Equipment →